01
Tool class
Match steel / aluminum to shot count and texture
HC-Mold capability · Dongguan
Rapid tooling lets teams mold real thermoplastics earlier. HC-Mold machines aluminum and soft-steel cavities for pilot molding, then supports the hand-off to production steel when volumes and cosmetics justify the spend.
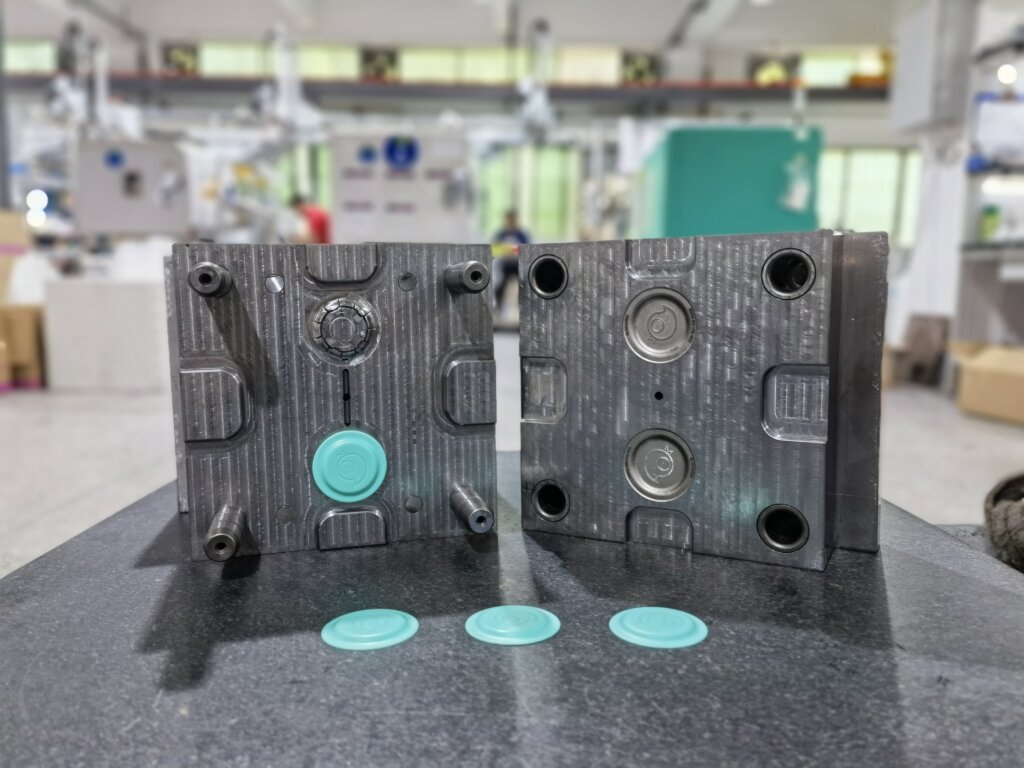
Match steel / aluminum to shot count and texture
Cavity, gate and cooling designed for the pilot plan
Approve samples; open hard tool or extend bridge
Tool steels and aluminum grades selected for the expected shot count. Production resin is the same family you intend for volume — that is the point of rapid tooling.
STEP/IGES/PDF drawings, material callout, volume band, finish target and ship-to region.
Engineering review with process recommendation, risk notes and lead-time options — no instant-CAD black box.
In-process checks, outgoing reports and export packaging from the Chang’an campus.
If annual volume, multi-cavity economics and cosmetics already demand hardened steel, we may recommend going straight to production tooling after DFM — and say so in the quote.
Ownership and storage terms are written into the PO. Soft tools typically remain in our Dongguan plant for follow-on pilots unless export is requested.
3-, 4- and 5-axis milling plus turning for aluminum, stainless, steel, brass and engineering plastics — from first article to repeatable lots.
Soft tools through hardened production molds, with DFM, mold trials and export packing from one Dongguan factory.
Laser cutting, CNC bending, punching, welding and finishing for enclosures, brackets and short-run fabrications.
Send drawings for DFM notes and a dated quote window from HC-Mold engineering.
Contact engineering